How to Test Parts Before Shipment: Pre-Shipment Inspection Checklist and 7-Step Process
 Import Export
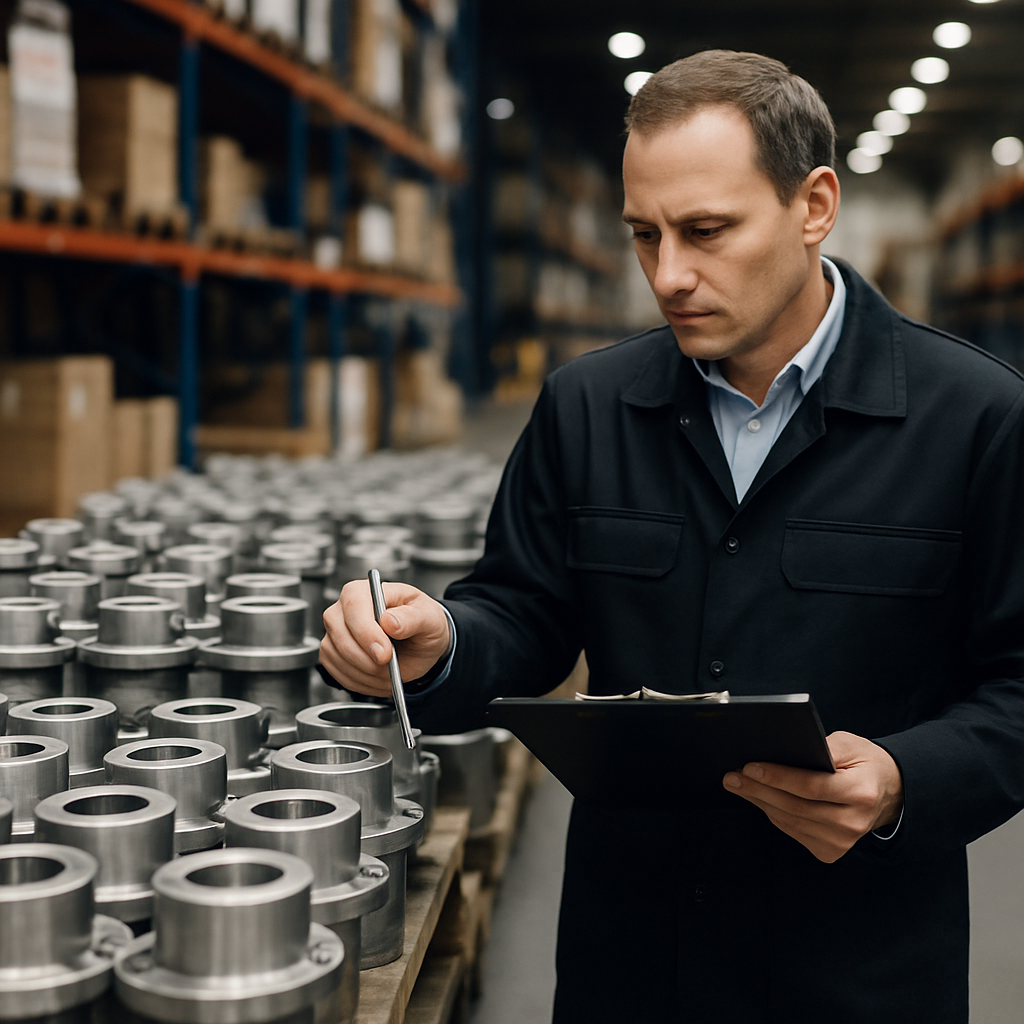
To test the quality of parts before shipment, verify that the finished order conforms to the requirements agreed with the supplier before it leaves the factory. This is normally done through a pre-shipment inspection (PSI), also called a final inspection or, in some programmes, a final random inspection. It checks the order against the purchase order and agreed specifications, including quantity, workmanship, dimensions where relevant, function, packaging, and applicable safety basics.
A PSI is not proof that every unit is defect-free, nor is it a substitute for product certification, laboratory testing, or destination-market compliance obligations. Its practical value is that it can identify non-conformities while the parts are still under the manufacturer's control, when rework, replacement, sorting, or a shipment hold may still be possible.
What It Means to Test Parts Before Shipment
A pre-shipment inspection is an on-site evaluation of finished or nearly finished goods before dispatch. QIMA describes PSI as a final quality check performed when production is at least 80% complete, covering quantity, quality, packaging, and safety basics. Other providers describe the inspection as taking place when roughly 80% to 100% of the order has been made and export-packed. The appropriate booking point should be agreed with the supplier and inspection provider so that enough completed goods are available for the planned sample.
The purpose is to determine whether the lot conforms to the buyer's agreed requirements before dispatch. In practice, that means checking more than general appearance. The inspection should compare the actual parts, order quantity, configuration, test results, labels, and packing with the requirements that applied when the order was placed.
A supplier's internal quality-control report can be useful, but it is not the same as an independent inspection. A buyer may choose a trained third-party inspector for an objective view of the lot rather than relying solely on supplier self-reporting. That does not mean third-party inspection is mandatory, or that suppliers should not conduct internal checks; it is a risk-control choice that should reflect the product, supplier relationship, and consequences of a defect.
Set the Standard Before Anyone Inspects the Parts
An inspection can only establish conformance if there is a clear baseline for comparison. Before the inspection is booked, provide the inspector and supplier with the same controlled requirements. The goal is to avoid a dispute in which the buyer expects one standard while the inspector can verify only a vague description.
The baseline should normally include the purchase order and any applicable approved drawings, specifications, samples, packaging instructions, and stated safety or compliance requirements. For each part or configuration, make the requirements inspectable rather than subjective.
- Part number, model, revision, material, and configuration.
- Dimensions, weights, and tolerances where relevant.
- Required components, assembly condition, markings, labels, and finish or workmanship expectations.
- Product-specific functional test method and expected result.
- Ordered quantity, carton count, packing configuration, and export-packaging requirements.
- Any agreed safety, regulatory, or destination-market requirements that need checking.
Before inspection begins, document the lot size, inspection level or sample plan, defect categories, acceptance numbers, and the person authorised to decide the disposition. The pre-shipment inspection guidance from Lifa Sourcing similarly stresses recording the lot size, sample plan, defect classes, acceptance numbers, and disposition owner in advance.
Legal and market-access requirements are product- and transaction-specific. Verify requirements for the exact part, origin, destination, and sales channel. A factory inspection may confirm agreed visible, dimensional, functional, or packaging criteria, but it does not automatically establish full regulatory compliance or replace required accredited testing.
Use a Sampling Plan Instead of Checking Parts at Random
Many PSI programmes use acceptance sampling: an inspector selects a defined sample from the lot and evaluates it against an agreed plan rather than examining every item. PSI providers commonly refer to AQL-based sampling and ISO 2859-1 or ANSI/ASQ Z1.4-style procedures. For example, Tetra Inspection explains that its PSI process uses AQL sampling under ISO 2859-1 to assess finished goods, specifications, and packaging.
AQL, or Acceptance Quality Limit, should be understood as part of an agreed acceptance-sampling approach. It is not a guarantee that every individual part in a passed shipment is defect-free. The sampling plan, lot size, inspection level, defect classifications, acceptance numbers, and decision rights all affect how the result is interpreted.
Classify defects before looking at the sample
A common framework groups defects as critical, major, or minor. The parties should define these categories for the actual parts and their intended use before inspection.
- Critical defects are generally defects with serious safety, legal, or essential-function implications under the agreed requirements.
- Major defects are generally defects likely to make a part unacceptable for its intended use, materially impair function, or depart significantly from specification.
- Minor defects are generally smaller departures from agreed appearance, finish, or workmanship requirements that do not materially affect use.
The agreed acceptance rules determine whether findings lead to a pass, fail, hold, or escalation. Do not select a universal AQL level or copy a sampling table without confirming that it suits the product and contract. High-risk, safety-critical, regulated, precision, or high-value parts may need stricter sampling, 100% sorting, specialised testing, or technical review rather than a standard final random sample.
What to Check When Testing Parts Before Shipment
Quality is not one check. A useful pre-shipment inspection checklist separates each verification activity, identifies the evidence or tool required, and records the agreed comparison baseline. The checklist below is suitable for saving or printing for internal use; it is not a universal substitute for a product-specific inspection plan.
| Check category | Evidence or tool needed | Comparison baseline | If non-conforming |
|---|---|---|---|
| Quantity and lot identity | Count records, carton count, order documents, and part identification | Purchase order, ordered quantity, and approved part or configuration | Record shortages, overages, mixed models, or unidentified goods; hold or clarify the shipment as agreed. |
| Visual appearance and workmanship | Visual examination, approved sample, finish standard, and defect definitions | Agreed appearance, assembly, surface, and workmanship requirements | Classify scratches, surface issues, incorrect assembly, missing parts, or other defects under the agreed rules. |
| Dimensions and weight | Appropriate measuring equipment and recorded results | Approved drawing, specification, or stated dimensional requirement | Document measurements outside the agreed tolerance or other specified limit. |
| Function | Product-specific test equipment, method, and test record | Agreed functional requirement and test method | Document failures, conditions, and affected sample units; escalate where the test result affects use. |
| Safety basics, where applicable | Relevant inspection method and stated safety criteria | Agreed mechanical or electrical safety requirements | Escalate safety-related findings; a basic PSI is not full certification or laboratory testing. |
| Packaging, marking, and export-pack readiness | Packing instructions, labels, carton markings, and packaging-condition check | Agreed packing configuration and shipment requirements | Record incorrect labels, inadequate protection, wrong pack count, damaged cartons, or other deviations. |
Quantity and identity verification
Start by confirming that the lot presented for inspection matches the order. Compare the counted goods and cartons with the ordered quantity, and check relevant part numbers, model identifiers, revisions, or configurations. This helps identify shortages, mixed products, or a mismatch between the inspected lot and the order intended for dispatch.
Visual and workmanship checks
Inspect sampled parts for visible flaws and deviations from agreed workmanship requirements. Depending on the product, this can include surface defects, incorrect assembly, missing components, poor finish, damage, incorrect marking, or inconsistent appearance. The finding should be described against the approved requirement and classified using the agreed critical, major, or minor categories, not merely labelled as “poor quality”.
Specification and dimensional verification
Measure the characteristics that matter to fit, performance, handling, or the contract specification. This may include length, width, height, weight, or another stated dimension. Use an appropriate method and compare the result with the buyer's documented requirement. Do not invent generic tolerances: tolerances and measurement methods must come from the applicable drawing, specification, or approved standard.
Functional and safety-basics checks
Where a part has a functional requirement, test it using the agreed method. A functional check for an electrical component, mechanical assembly, garment fastening, or precision part will not be the same, so the test must be product-specific. Applicable mechanical or electrical safety basics may also be checked. As Easyship's PSI overview notes, relevant inspections can include dimensional verification, functionality verification, and mechanical or electrical safety checks.
These checks should not be represented as full safety certification, accredited laboratory testing, or proof that all statutory requirements have been met. If a product needs specialist performance, chemical, electrical, or compliance testing, specify that work separately.
Packaging and export-packaging readiness
Check that packaging is correct, in suitable condition, and configured as agreed to protect the parts during shipment. Where required by the order, verify labels, marks, carton contents, pack count, and packing configuration. Product packaging checks during PSI are distinct from arranging cargo restraint for transport. For the latter stage, see these cargo-securing and industrial packaging considerations.
A Practical 7-Step Inspection Process Before Shipment
There is no single universal seven-step inspection sequence for every product or inspection provider. The following is a practical PSI workflow that brings the main checks into a usable order. Adapt it to the part, contract, risk level, and agreed test methods.
- Define the scope and acceptance criteria. Issue the purchase order, specifications, drawings or approved samples where applicable, packaging instructions, relevant requirements, defect definitions, and decision authority.
- Confirm production readiness and schedule the inspection. Ensure the goods are sufficiently complete for a meaningful inspection. PSI is commonly scheduled when roughly 80% to 100% of production is complete, often once goods are finished and export-packed.
- Identify the lot and establish the sampling plan. Record the lot size, inspection level, sample plan, defect classes, acceptance numbers, and AQL or other agreed acceptance basis where used.
- Verify quantity and basic order identity. Check the available quantity, carton count, relevant part or model identifiers, and configuration against the agreed order.
- Inspect appearance and workmanship. Examine the selected sample for visible defects, missing components, incorrect assembly, finish issues, and other stated quality requirements.
- Conduct applicable dimensional, functional, and safety-basics checks. Measure and test only against agreed specifications and methods, documenting the tools, conditions, and results where relevant.
- Inspect packaging, document findings, and decide the disposition. Confirm packaging readiness, classify defects, compile the report, and follow the agreed path: release, hold, rework, replacement, sorting, reinspection, or escalation.
Define the final decision-maker and corrective-action route before the visit. An inspector's report records findings and may include a pass/fail recommendation under the agreed criteria, but it is not automatically a binding commercial instruction unless the buyer's contract makes it one.
Who Checks Product Quality Before Shipment?
Pre-shipment checks can be performed by trained inspectors, often through an inspection company selected by the importer or buyer. The buyer may arrange and pay for the service, while the inspector visits the manufacturing site, examines the goods, and reports the findings. QCADVISOR describes PSI as a structured process carried out by trained inspectors to assess whether goods meet the buyer's stated requirements.
The supplier can and should carry out internal quality control, but an independently selected inspector can give the buyer a separate assessment of the lot. Independence is particularly useful where the buyer cannot visit the factory, the order is technically important, or the cost of receiving defective parts would be high.
Keep the roles clear. The inspector assesses and documents conformance or defects. The buyer and supplier should agree who has authority to release the shipment, approve a concession, order rework, require replacement, authorise sorting, or accept a deviation. This prevents an inspection report from becoming an unclear substitute for commercial decision-making.
What to Do When the Inspection Finds Problems
The report should provide enough detail for a defensible shipment decision. It should normally state what was checked, the lot and sample quantity or plan, defects found, defect category, relevant photos or measurements where available, and the resulting recommendation or disposition. A vague statement that an order “failed quality control” is rarely enough to manage correction with a supplier.
Possible responses depend on the agreement and severity of the findings:
- Pass and release: release the shipment when the result meets the agreed acceptance criteria.
- Hold pending clarification: pause dispatch while quantity, identity, documentation, or a disputed finding is reviewed.
- Rework and reinspect: require correction, then inspect the corrected lot before release.
- Replace affected goods: request replacement when rework is unsuitable or the parts do not conform.
- Sort or conduct 100% screening: use a stricter check where the risk and defect pattern justify it.
- Escalate for a buyer decision: refer a commercial, technical, safety, or contractual issue to the authorised decision-maker.
Finding problems before dispatch can prevent defective or unsellable goods from entering the transport chain and may reduce the disruption associated with returns, delays, and customer dissatisfaction. It also gives the supplier an opportunity to correct the issue while the goods remain at the factory.
Some providers issue a pre-shipment inspection certificate. However, a PSI certificate is not universally required, and it does not automatically satisfy customs requirements in every market. Verify any inspection, certification, or import-document rule for the exact product, origin, destination, and transaction. A successful PSI is also separate from preparing shipping and customs documents, including the commercial invoice requirements for international shipping.
Use PSI as a Release Control, Not a Paper Exercise
The strongest pre-shipment inspection process connects a clear specification to an agreed sample plan, product-specific checks, evidence-based reporting, and a defined shipment-release decision. Test the quality of parts before shipment against what was actually agreed, rather than relying on broad assurances that the goods are “good” or “ready”.
For routine, low-risk orders, a standard sampled PSI may provide a proportionate final check. For precision, regulated, safety-critical, high-value, or repeatedly problematic parts, consider whether the order needs tighter controls before dispatch, such as specialised tests, technical review, 100% screening, or reinspection after corrective action. The appropriate control is the one that matches the product risk and gives the buyer a clear basis to release, hold, or correct the shipment.